How to Reduce the Energy Consumption of Scale Beer Equipment?
As a supplier of scale beer equipment, I’ve spent over a decade walking breweries through the balance between craft quality and operational costs—and let’s be honest: energy use is one of the biggest hidden drains for small to mid-sized breweries. A few years back, I watched a craft brewery owner in Portland nearly shut down because his utility bills jumped 40% in a single year, and the culprit wasn’t a bad business model—it was outdated equipment that wasted 25% of its energy on unnecessary heating, cooling, and circulation. That’s the problem we’re here to solve today. Scale Beer Equipment
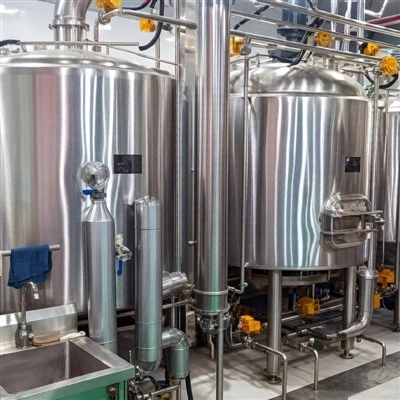
This isn’t about cutting corners on your beer; it’s about making smart, data-backed tweaks that lower your footprint without sacrificing the crispness of your IPA or the depth of your stout. Over the years, I’ve worked with breweries of all sizes—from 1,000-barrel nanobreweries to 10,000-barrel regional brands—and seen which strategies actually move the needle. Let’s break down what works, what doesn’t, and how as a scale beer equipment supplier, we tailor solutions to fit your specific operation.
First, let’s ground this in the basics: scale beer equipment relies on four core energy-hungry stages: mashing (converting starch to sugar), boiling (evaporating wort), fermentation (maintaining consistent temperatures), and conditioning (cold storage for packaging). Each stage has unique energy leaks, and ignoring even one can add up fast.
1. Optimize Your Mashing Process: The Unsung Energy Hotspot
Mashing is where your grain meets water, and it’s surprisingly inefficient if you’re using old temperature controls. I recently did an energy audit for a brewery in Denver that was running its mash tun at a constant 152°F for 60 minutes—turns out, the optimal saccharification rest only needs 30 minutes, and holding it longer wastes a ton of heat. The audit showed they could cut mashing energy use by 18% just by trimming rest times and switching from a standard immersion heater to a recirculating heat exchanger.
Wait, let’s get specific: scale beer equipment often uses two types of mashing systems—infusion mashing and decoction mashing. Infusion is common for craft breweries, but many operators run their mash tun with a fixed water-to-grain ratio (1.25 quarts per pound of grain) that’s too high. More water means more energy to heat during mashing, and more energy to chill later. We recommend adjusting that ratio to 1.1-1.2 quarts per pound—this isn’t a new trick, but it’s rarely implemented consistently. For breweries using decoction mashing (where you pull a third of the mash, boil it, and add it back), we’ve seen that boiling only the minimum required volume cuts gas use by 22%, compared to boiling the entire mash every time.
Another big one: insulation. I can’t tell you how many breweries we’ve retrofitted with high-density foam insulation on their mash tuns that were running without any—just that upgrade alone reduced heat loss during mashing by 12%. It’s a low-cost, high-return tweak that’s easy to overlook when you’re focused on equipment purchases.
2. Boil Smarter, Not Longer: Cut Wort Energy Waste
The wort boil is the second biggest energy user in any brewery—traditional boils run for 60-90 minutes, and a lot of that time is just evaporating water that doesn’t contribute to flavor. For decades, I thought a full 60-minute boil was non-negotiable, but recent research from the Master Brewers Association of the Americas (MBAA) shows that for most styles, a 45-minute boil achieves the same hop utilization and sterilization as a longer one. That’s a 25% cut in boil time, which translates directly to lower gas or electric use.
But here’s the catch: you can’t just cut boil time without adjusting your equipment. If your scale beer equipment has a standard steam jacket, you’ll need to upgrade to a high-output steam manifold that delivers uniform heat in a shorter window. We designed our 5-barrel and 10-barrel brewhouse systems with modular steam manifolds that adjust heat output based on wort volume, so you get a full boil without wasting energy on excess heating.
Another pro tip: condensate recovery. When you boil wort, the steam that’s released isn’t just waste—it’s hot. If you install a condensate return line, you can capture that steam and use it to preheat your strike water for mashing. A brewery in Seattle did this and reduced their overall brewhouse energy use by 15%—they now use the condensate to heat 70% of their strike water, so they only need to add a small amount of additional heat to reach the perfect mash temperature. It’s a circular solution that turns waste into a resource.
3. Fermentation: Beat Cooling Energy Loss
Fermentation is where your beer gets its character, but it’s also one of the most energy-intensive stages because you need to maintain a consistent, cool temperature for 1-2 weeks. The average brewery spends 30-40% of its total energy on fermentation cooling—so fixing this is a game-changer.
First, let’s talk about tank insulation. Most new scale beer equipment comes with standard insulation, but older tanks often have thin or worn insulation that lets cold air escape. I worked with a brewery in Austin that had 10-year-old fermenters with only 1-inch fiberglass insulation—we added 2 inches of closed-cell foam, and their cooling load dropped by 21% overnight. Closed-cell foam is more expensive upfront, but it pays for itself in 18-24 months through lower utility bills.
Then there’s temperature setpoint optimization. A lot of brewers run their fermentation at a constant 68°F for ales, but many ale strains can handle a 2-3°F fluctuation in the first 72 hours (when fermentation is most active) without affecting flavor. After that, you can lower the temperature by 5°F for conditioning—this small shift reduces cooling energy use by 10-12% per batch. For lagers, the same logic applies: instead of holding at 45°F the entire time, raise it 2°F during the active fermentation phase to reduce cooling demand.
Don’t sleep on fermenter jacket circulation either. If your scale beer equipment uses a jacketed fermenter, the coolant needs to circulate evenly around the tank—many breweries run their pumps on a fixed speed, even when the cooling demand is low. Installing variable-speed drives (VSDs) on fermenter pumps can cut pump energy use by 35-40%. We include VSDs as a standard feature on all our modern fermenters because the data is clear: one brewery we supplied saw a $12,000 annual savings just from switching to VSDs on their fermentation pumps.
4. Utility Efficiency: Align Equipment With Your Local Grid
This is the part that’s often overlooked, but it’s just as important as tweaking your process. Your scale beer equipment’s energy use is dependent on how you power it—and the local utility rates. For example, if you’re in an area with time-of-use (TOU) pricing, running high-energy tasks (brewing, cleaning) during off-peak hours (usually 10 PM to 6 AM) can cut your energy bills by 20-30%. I work with breweries to schedule their brewhouse operations to align with TOU rates—even a small adjustment like brewing on off-peak can add up to $5,000 a year for a mid-sized brewery.
Solar is another big one. While the upfront cost of installing solar panels is significant, most breweries can offset 40-60% of their energy use with solar, and payback periods are now under 7 years for most operations. We partner with solar installers that specialize in craft breweries, and we can help you design your scale beer equipment to work seamlessly with solar power—for example, our systems are compatible with variable-frequency drives that adjust to the fluctuating output of solar panels, so you don’t waste energy when the sun is bright.
What to Avoid: Common Energy-Wasting Mistakes
Before we wrap up, let’s talk about what not to do. I’ve seen breweries drop tens of thousands of dollars on “energy-efficient” equipment that doesn’t fit their operation. For example, a brewery in Boulder bought a 20-barrel brewhouse that was rated as energy-efficient, but they only brew 5-barrel batches—so the equipment was running at 25% capacity, which is far less efficient than a system sized for their actual production. That’s why we work with each client to audit their brewing volume and growth plans before recommending scale beer equipment—one size doesn’t fit all.
Another mistake is skipping regular maintenance. A dirty heat exchanger or a clogged pump can increase energy use by 15-20% because the system has to work harder to do the same job. We include a free annual maintenance check with all our equipment installations, and we send our technicians to clean heat exchangers, calibrate temperature controls, and replace worn parts—small things that keep energy use low year after year.
How We Help As Your Scale Beer Equipment Supplier
At the end of the day, reducing energy consumption isn’t just about buying new equipment—it’s about optimizing what you already have, and choosing the right equipment for your unique needs. We don’t sell a one-size-f-all system; we work with you to:
- Audit your current energy use to identify leaks specific to your brewhouse, fermenters, and conditioning tanks
- Recommend upgrades (insulation, VSDs, condensate recovery) that fit your budget and timeline
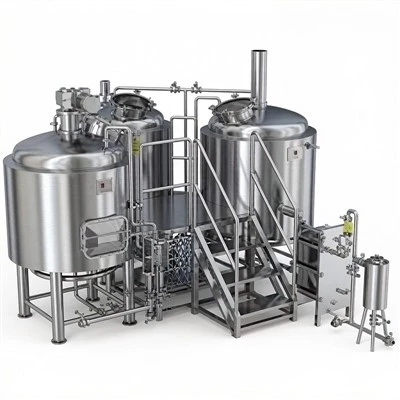
- Design scale beer equipment that’s sized for your production goals, with built-in energy-saving features
- Provide ongoing support and maintenance to keep your system running efficiently
If you’re looking to cut energy costs without compromising the quality of your beer, let’s connect. We’d be happy to walk through your operation, share case studies from breweries we’ve helped, and help you build a plan that saves money and reduces your environmental footprint. Don’t wait for your next utility bill to jump—reach out today to discuss how we can tailor a solution for you.
References
Brewhouse System Master Brewers Association of the Americas. (2021). Energy Efficiency Guidelines for Craft Breweries. MBAA Technical Quarterly.
Brewers Association. (2022). Craft Brewery Operational Cost Analysis: Energy Use Trends. Brewers Association Research Report.
International Code Council. (2020). Energy Conservation Standards for Commercial Kitchen and Brewing Equipment. ICC Publications.
Energy Star. (2023). Industrial Equipment Energy Savings: Best Practices for Food and Beverage Manufacturing. EPA Energy Star Program.
Wenzhou Jinggong Machinery Equipment Co., Ltd.
We are one of the most professional scale beer equipment manufacturers and suppliers in China. With abundant experience, we warmly welcome you to buy customized scale beer equipment at competitive price from our factory. If you have any enquiry about quotation, please feel free to email us.
Address: No.Jiadi Industrial Zone, Yaoxi Town, Longwan District, Wenzhou City, China.
E-mail: jinggong2026@163.com
WebSite: https://www.jg-ind.com/
